Custom Machined Sleeve with Tapered Profile and Side Cutout
- Part No :
-
- Product Type: Custom Machined Sleeve
- Manufacturing Process: CNC Turning
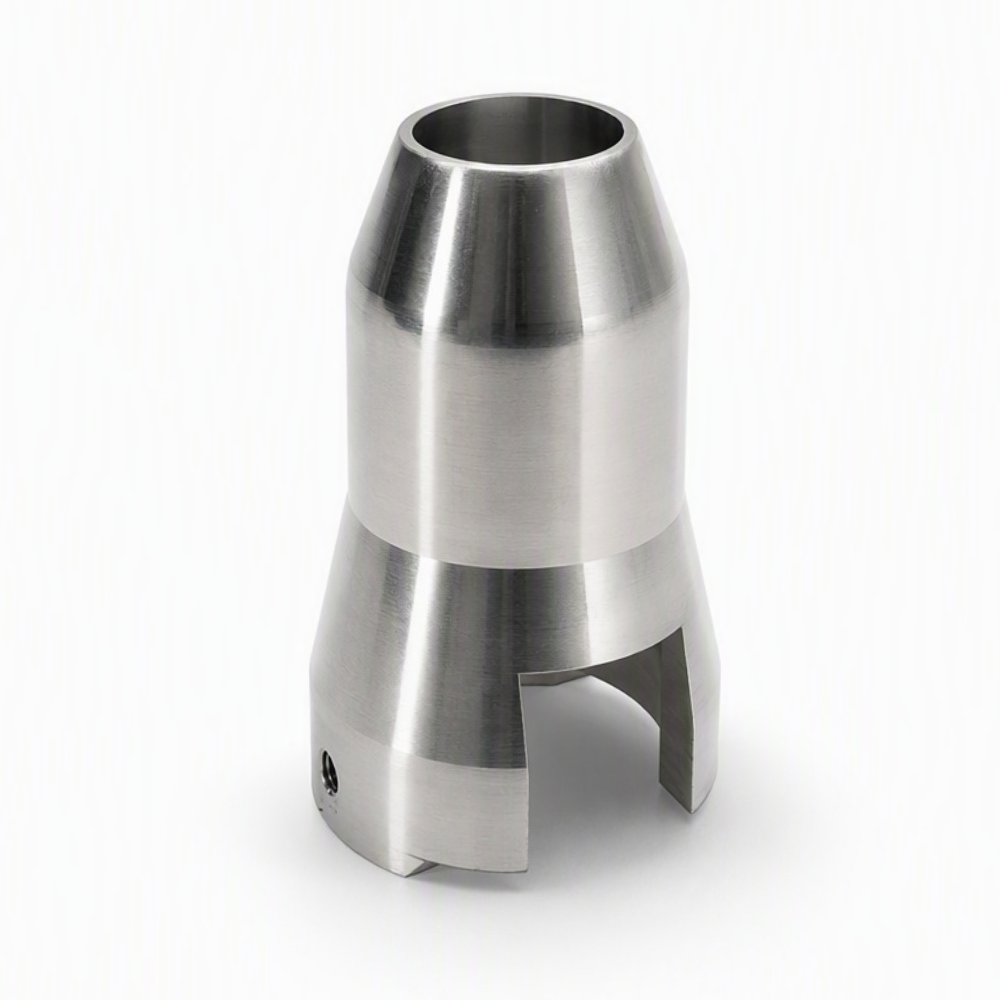
- Structure: Axial Opening, Tapered Outer Sections, Cylindrical Band, Lower Side Cutout and Small Side Hole
- Material Options: Stainless Steel, Carbon or Alloy Steel, Aluminum Alloy or Brass
- Surface Finish Options: Material-Compatible Machined, Passivated, Plated or Anodized Finishes
- Bore, Profile and Cutout: Customized to Drawing
- Side-Hole Requirements: According to Drawing
- Tolerances and Inspection: According to Drawing Requirements
- Production Type: Made to Order
- Quotation Inputs: Drawing, Material Grade, Mating Geometry, Finish, Inspection Requirements and Quantity
- Inquiry now
Detailed description
This custom machined sleeve combines a visible axial opening, tapered outer sections, a cylindrical middle band, a lower side cutout and a small side hole. LAMBOOR supplies the turned component to customer drawings, with the profile and interfaces configured for the mating assembly. The bore layout, side-hole specification and function are defined by the design rather than a standard catalog size.
Typical Turning and Feature Preparation
A typical route starts with a drawing review and a suitable blank. Facing, external turning and internal machining establish the main axis, cylindrical surfaces and tapered profile. The manufacturing plan then addresses the cutout and side-hole features while preserving the required wall sections and reference relationships. Their detailed operations depend on the approved drawing. Deburring, cleaning, compatible surface treatment and final inspection complete the route.
Structure-Specific Manufacturing Priorities
- Bore and outer profile: Define the relationship between the internal interface and external locating surfaces, including the required geometric controls.
- Interrupted lower wall: The side cutout reduces local support. Workholding and inspection should account for distortion and avoid damaging the remaining edges.
- Taper transitions: Specify taper angle or defined diameters and lengths, together with radii and edge breaks that affect assembly.
- Intersecting features: Remove burrs where the cutout or hole meets an internal surface, without rounding a functional edge beyond its drawing requirement.
Material Options
Options include stainless steel for corrosion-focused requirements, carbon or alloy steel for strength and wear considerations, aluminum alloys where weight matters, and brass where machinability or specific electrical requirements favor it. Select the actual grade and condition according to loads, contact materials, service environment and cost. Remaining wall thickness around the opening must be assessed as part of the design, not inferred from the photograph.
Compatible Surface Finishes
As-machined surfaces can be retained where suitable. Stainless steel may be passivated or electropolished; aluminum can use anodizing, hard anodizing or bead blasting with an appropriate dimensional allowance. Carbon and alloy steels can use suitable plating, phosphating or black oxide. Black oxide requires appropriate supplementary corrosion protection, and high-strength steel plating may need hydrogen-embrittlement controls.
Specify finish coverage and masking on the bore, tapered interfaces and small side hole. Coating accumulation around internal edges or the cutout can affect fit and clearance. Thick powder coating is unsuitable for an unmasked precision bore. Appearance and surface-roughness acceptance should be defined separately when they serve different purposes.
Drawing-Controlled Inspection
The drawing establishes the internal depth and profile, outside diameters, taper, cutout shape, hole details and edge treatment. Mark the functional datums, geometric tolerances, inspection condition after treatment and any reporting requirements. Include internal-edge cleanliness and accessible inspection locations where the cutout or hole creates an interrupted surface.
FAQ
Does the side cutout make this sleeve a collet or clamping component?
Not by itself. An open section does not establish a clamping function, allowable deflection or grip performance. Provide the mating arrangement and required movement or load conditions if clamping is intended. The design and validation requirements must define that function rather than treating the cutout as a performance specification.
Should the sleeve bore be specified as blind or through?
Yes, the drawing should state the complete bore layout. Specify depth, internal steps, end conditions and any connection to the cutout or side hole. A visible opening does not define the far end. These details affect mating-part insertion, available clearance and how the internal features can be inspected.
How can a part that moves past the cutout avoid catching an edge?
Define the movement envelope and the required edge break or radius at the cutout. Include acceptable burr condition and clearance throughout the travel, not just at one position. Where the edge also serves as a stop or locator, distinguish that controlled contact edge from surfaces that should be relieved.
Request a Quotation
Provide a dimensioned drawing and available 3D model, material grade, finish, quantity and inspection requirements. Show the complete internal geometry and mating arrangement, with critical clearances, side-hole details and any sample-approval or packaging requirements.